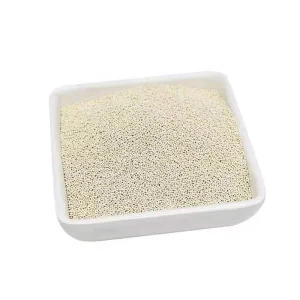
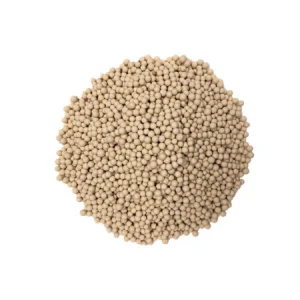
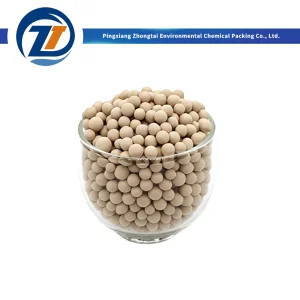
Precision-engineered Zeolite 3A, 4A, 5A, and 13X Molecular Sieves formulated to accelerate downstream natural gas processing, LNG liquefaction, syngas refining, and cryo-air separation across Tashkent, Navoi, and Bukhara.
Engineered for high mass transfer, exceptional crush resistance, and minimal hydrothermal degradation under demanding desulfurization and deep drying cycles.
With an annual natural gas extraction capacity surpassing 50 billion cubic meters and massive capital injections into downstream Gas-to-Chemicals (MTO) and Gas-to-Liquids (GTL) projects in the Kashkadarya, Bukhara, and Navoi regions, Uzbekistan stands as Central Asia’s central hub for processing technologies.
Complex natural gas reserves containing sour gas (H₂S) and high carbon dioxide concentrations mandate severe dehydration to sub-ppm levels (<0.1 ppmv H₂O) prior to cryogenic turbo-expansion, stopping hydrate formation in pipelines leading to Europe and China.
Navoiyazot and Ferganaazot modernization plans demand hundreds of metric tons of type 4A, 5A, and 13X APG molecular sieves for PSA hydrogen recovery, ammonia synthesis loops, and pre-purification units (PPU) running continuous thermal swing adsorption (TSA).
Direct freight access via the China-Kyrgyzstan-Uzbekistan cross-border trade framework and the China Railway Express provides transit turnaround times within 12 to 18 days, significantly minimizing supply line vulnerabilities compared to European seaborne freight.
Choosing proper framework geometry and cation-exchanged pore apertures ensures longevity and avoids hydrocarbon co-adsorption in process streams.
| Zeolite Crystal System | Pore Window & Cation | Typical Critical Duty | Hydrocarbon Selectivity | Key Performance Indicators |
|---|---|---|---|---|
| Type 3A (KA) | ~3.0 Å (Potassium K+) | Cracked gas, ethylene, LNG feed stream dehydration | Excludes all hydrocarbons >3Å (prevents co-adsorption fouling) | Water Uptake ≥ 21.0% · Crush Strength ≥ 35 N (1.6-2.5mm) |
| Type 4A (NaA) | ~4.0 Å (Sodium Na+) | Closed-loop instrument air, natural gas pipe-end drying | Adsorbs water, CO₂, H₂S; excludes propane and larger fractions | Bulk Density ~0.72 g/ml · Static H₂O Capacity ≥ 21.5% |
| Type 5A (CaA) | ~5.0 Å (Calcium Ca2+) | Normal/iso-paraffin separation, PSA H₂ refining | Separates straight-chain hydrocarbons from branched configurations | Purity Recovery >99.99% · Low attrition rate ≤ 0.15% |
| Type 13X / 13X APG (NaX) | ~10.0 Å (Faujasite) | Cryogenic air prepurification, mercaptan & H₂S sweetening | High co-adsorption capacity for polar aromatics, H₂O, CO₂ | CO₂ Adsorption ≥ 18 mg/g at ambient dynamic breakthrough |
Combining the natural raw mineral benefits of Pingxiang's chemical packing cluster with rigorous process automation delivers reproducible adsorption beds at realistic cost structures.
Continuous rotary calcination ensures consistent thermal profile across every batch, achieving zero crystalline phase destruction and homogeneous pore opening dimensions.
Every lot is quantified for LOI (Loss on Ignition), static and dynamic adsorption breakthrough, and single-pellet crush rating prior to container sealing.
We provide full customs processing for bonded rail shipments directly delivered to Tashkent (Sergeli station) or Samarkand under clean CIP terms.
Real-world integration of high-performance zeolites inside severe operational conditions.
At regional peak shaving gas plants and export LNG units, trace water vapor results in crystalline ice and clathrate blockages across cold boxes operating at -160°C. Deploying low-dusting Zeolite 3A reduces bed dusting attrition and sustains stable pressure drops across multi-year swing cycles.
Modern steelmaking and synthesis operations require extensive tonnage oxygen and nitrogen. 13X APG molecular sieve beds eliminate CO₂ and acetylene down to <0.5 ppm, preventing catastrophic crystallizing in cryogenic main condensers and ensuring explosive hydrocarbons do not accumulate.
Targeted technical details resolving import requirements, packaging integrity, and dynamic longevity.
Complete product spectrum covering cryogenic separation, high-pressure natural gas drying, and industrial tower mass transfer internals.