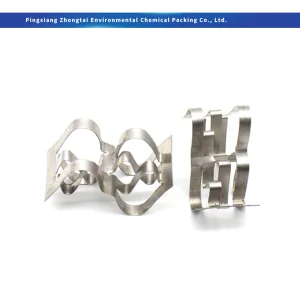
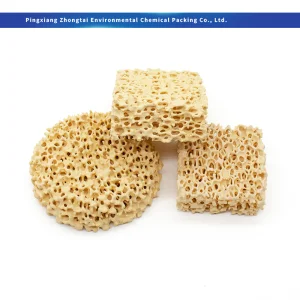
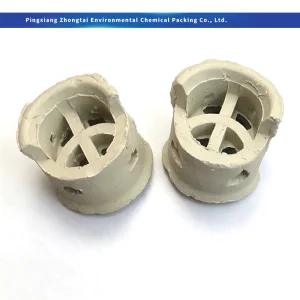
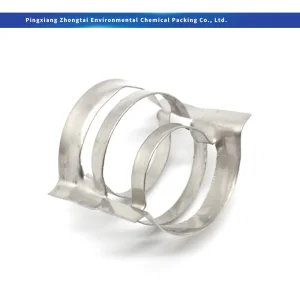
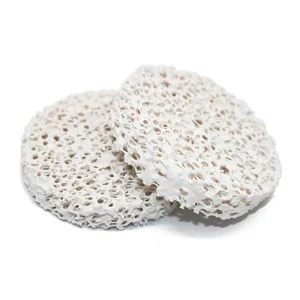
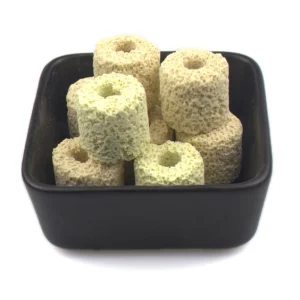
Engineered mass transfer components designed for high gas velocity, minimized pressure drop, and severe chemical corrosion endurance.
Strategic analysis of mass-transfer dynamics, thermal stability in aggressive media, and cross-continent manufacturing economics.
In modern chemical engineering, mass transfer columns remain central to critical separation, absorption, and stripping operations. Despite rapid advancements in structured packings and specialized high-alloy metallic internals, Ceramic Random Packing maintains irreplaceable superiority across corrosive, high-temperature, and oxidatively hostile chemical environments. Global installations in sulfuric acid manufacture ($H_2SO_4$), coal gasification, sulfur recovery units (SRU Claus process), and acid-gas scrubbing towers consistently require chemical porcelain that provides complete acid resistance (except hydrofluoric acid) up to temperatures exceeding 1000°C.
Historically dominated by early designs such as standard Raschig Rings, the industry has migrated toward advanced second- and third-generation geometries including Ceramic Intalox Saddles, Ceramic Conjugate Rings, and Cascade Mini-Rings. These optimized structures alter internal gas-liquid routing, drastically reducing liquid hold-up and operational pressure drop ($\Delta P$), while eliminating stagnant pockets that catalyze column fouling or salt deposition.
Global petrochemical operators are actively replacing costly titanium and specialty nickel alloys with engineered ceramic random packings in hot acidic wash sections, yielding up to 65% reduction in packed column capital expenditures.
The global push toward carbon neutrality and industrial VOC emission abatement has accelerated demand for thermal-shock resistant ceramics like mullite and cordierite in regenerative thermal and catalytic oxidizers.
Sudden liquid quenching in absorption towers requires ceramic packing with ultra-low thermal expansion coefficients and high cold crushing strength to avoid mechanical degradation during unit startups and shutdowns.
Unrivaled manufacturing density, vertically integrated raw materials, and digital kiln operations since 2003.
Located in Pingxiang City, Jiangxi Province—internationally recognized as the "Ceramic Capital of Chemical Industrial Materials"—Pingxiang Zhongtai Environmental Chemical Packing Co., Ltd. benefits from unique structural cluster efficiencies. High-purity kaolin clay reserves, feldspar deposits, and localized natural gas tunnel kilns reside within an ultra-short industrial perimeter. This geographic advantage eliminates long-distance transport costs for raw mineral powders, stabilizes raw-batch consistency, and delivers an unmatchable pricing framework to global buyers.
Our facility blends digital automated wet-extrusion presses, high-tonnage hydraulic molding systems, and computerized temperature-profile tunnel kilns firing up to 1350°C. This guarantees optimal vitrification, virtually zero open porosity, chemical inertness against concentrated sulfuric and hydrochloric acids, and exact mechanical dimensional consistency that prevents tower bed maldistribution.
Indicative FOB factory price metrics, physical properties, geometric characteristics, and packing factors for process engineers.
| Packing Model & Geometry | Available Sizes (mm / in) | Surface Area ($m^2/m^3$) | Free Volume ($\%$) | Bulk Density ($kg/m^3$) | Indicative Price (USD/m³ FOB) |
|---|---|---|---|---|---|
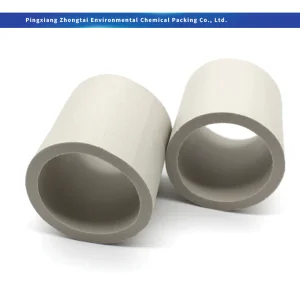
| Ceramic Raschig Ring | 16, 25, 38, 50, 76 mm | 100 – 310 | 68 – 75 | 550 – 720 | $140 – $240 / m³ |
| Ceramic Intalox Saddle | 25, 38, 50, 76 mm (1"–3") | 110 – 260 | 72 – 79 | 530 – 680 | $170 – $280 / m³ |
| Ceramic Conjugate Ring | 25, 38, 50, 76 mm | 130 – 280 | 74 – 81 | 500 – 620 | $190 – $310 / m³ |
| Ceramic Cascade Mini-Ring | 25, 38, 50 mm | 140 – 290 | 75 – 82 | 480 – 610 | $220 – $350 / m³ |
| Inert Ceramic Support Balls | 3mm to 50mm (1/8" to 2") | Specific to OD | 40 – 45 | 1350 – 1450 | $260 – $850 / MT |
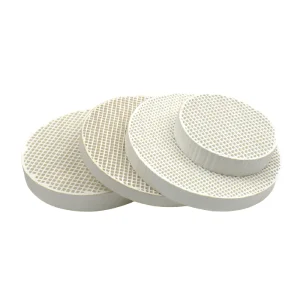
| Honeycomb Ceramic Blocks | 150×150×150 / 300 mm | Channel Dependent | 60 – 72 | 450 – 650 | $280 – $480 / m³ |
How Zhongtai media powers heavy process units worldwide and adapts to next-generation separation requirements.
Operating under 93% to 98% circulating sulfuric acid at elevated temperatures, ceramic Intalox saddles guarantee total resistance to hot acid wash, resisting disintegration, wall degradation, and bed compaction.
High soot-loading and variable gas flow demands robust ceramic Raschig rings and ceramic conjugate packing with high free volumes to bypass particulate plugging and maintain uninterrupted contact efficiency.
Modern column upgrades utilize micro-grooved and surface-treated ceramics that enhance liquid film spreading, lowering HETP (Height Equivalent to a Theoretical Plate) by up to 18% in high-vacuum distillations.
Meeting rigorous ASTM, ISO, and multinational EPC testing protocols prior to vessel charging.
Global procurement teams from Europe, North America, the Middle East, and Southeast Asia implement strict factory auditing protocols when qualifying a Chinese ceramic tower packing factory. At Zhongtai, every production heat conforms to ASTM C515 (Standard Specification for Chemical-Resistant Ceramic Tower Packings) and ISO 9001 certified manufacturing controls.
Crucial Factory Verification Parameters:
Authoritative technical clarifications addressing material selection, tower packing mechanics, and commercial logistics.
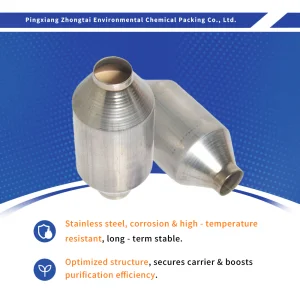
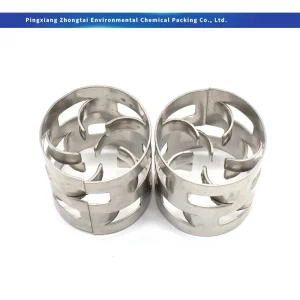
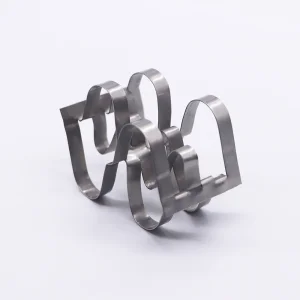
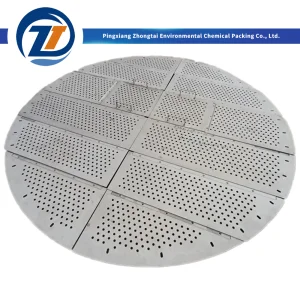
Comprehensive portfolio of metal, ceramic, and honeycomb media directly available from our Pingxiang manufacturing base.