Standard-setting precision random packing, molecular sieves, and catalytic components direct from Chinese industrial manufacturing clusters.
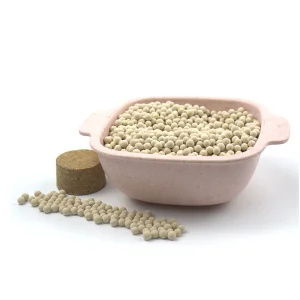
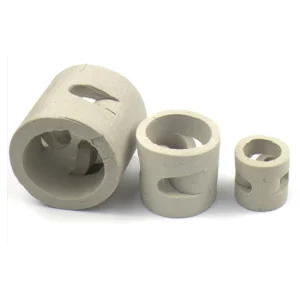
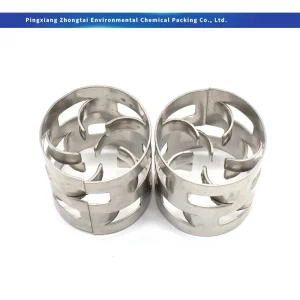
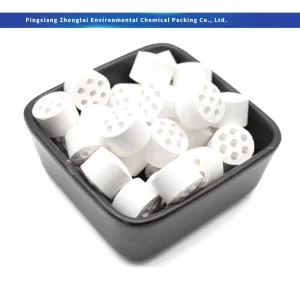
In the global transition toward sustainable biofuels, zero-carbon energy vectors, and ultra-pure chemical feeds, breaking the ethanol-water binary azeotrope (at 95.63 wt% ethanol and 4.37 wt% water) efficiently is an engineering imperative. Traditional azeotropic distillation relying on entrainers such as cyclohexane or benzene presents high thermal duties, environmental toxicity risks, and operational complexity. Modern bio-refineries overwhelmingly deploy Pressure Swing Adsorption (PSA) and Temperature Swing Adsorption (TSA) systems loaded with specialized 3A synthetic molecular sieves.
As a premier China Molecular Sieve Ethanol Manufacturer & Supplier, Pingxiang Zhongtai Environmental Chemical Packing Co., Ltd. synthesizes crystalline Type A aluminosilicates with controlled potassium ion exchange ($K_{12}[(AlO_2)_{12}(SiO_2)_{12}]\cdot nH_2O$). By maintaining an effective pore opening calibrated to exactly $3.0\text{ \AA}$, the crystal matrix easily admits water molecules (kinetic diameter $2.8\text{ \AA}$) while sterically excluding ethanol molecules ($4.4\text{ \AA}$). This precise molecular sieving mechanism prevents ethanol co-adsorption, maximizing working water capacity and drastically reducing energy loss during desorptive bed regeneration.
Next-generation vapor-phase dehydration frameworks demand extended hydro-thermal durability, lower pressure drop geometries, and integration with hybrid membrane separation modules.
Optimizing the K+ to Na+ exchange ratio controls the precise lattice constraint. A ratio tuned between 60% and 70% potassium substitution offers the ideal equilibrium: preventing ethanol entry while maximizing mass transfer coefficient and water kinetic uptake rates under 140°C–170°C vapor operating regimes.
Repeated cyclic pressure swings and high-temperature steam desorption induce lattice degradation over time. Our technological roadmap incorporates framework stabilization via rare-earth micro-doping, retaining >90% of initial static water sorption capacity after 15,000 thermal swing cycles.
The future of green bio-ethanol refining integrates NaA zeolite pervaporation membranes for bulk water removal (from 80% to 95% purity) followed by 3A molecular sieve PSA beds for polishing to 99.9%+. This hybrid approach reduces steam energy footprint per liter by up to 35%.
| Performance Parameter | Standard Commercial 3A | Zhongtai High-Purity Ethanol Grade 3A | Engineering Benefit |
|---|---|---|---|
| Nominal Pore Diameter | 3.2 Å – 3.5 Å | 3.0 Å (Strict Monodispersity) | Zero ethanol co-adsorption, reduced thermal spikes |
| Static Water Adsorption (25°C, 60% RH) | ≥ 20.5 wt% | ≥ 22.5 wt% | Smaller bed footprint, longer cycle times |
| Crush Strength (Spherical 3-5mm) | ≥ 65 N/bead | ≥ 85 N/bead | Eliminates bed compaction & dusting risk |
| Bulk Density | 0.68 - 0.72 g/mL | 0.72 - 0.76 g/mL | Optimized fluidization resistance in fast-swing PSA |
| Ethylene/Ether Formation Rate | < 0.05 wt% | < 0.008 wt% | Preserves ethanol volume yield; protects downstream equipment |
Tailored adsorption media and mass transfer internals designed for extreme industrial processing requirements.
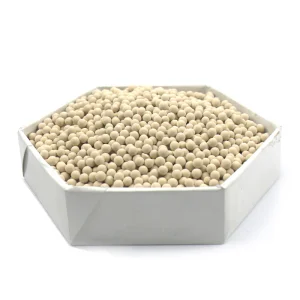
Large-scale grain and sugarcane biorefineries require continuous processing of high-volume alcohol vapors. Our 3A spherical adsorbents (typically 3-5 mm for lower beds, 2-3 mm for trim layers) guarantee fuel moisture levels under 0.5% (v/v) in accordance with ASTM D4806 and EN 15376 specifications.
For USP/EP grade extraction and formulation alcohols, trace chemical contaminants or secondary reaction by-products are strictly prohibited. Zhongtai’s ultra-pure 3A sieves prevent trace aldehyde or ester generation, maintaining original sensory and organoleptic properties required for medical extractions.
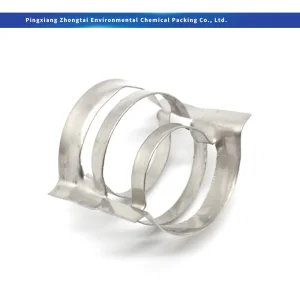
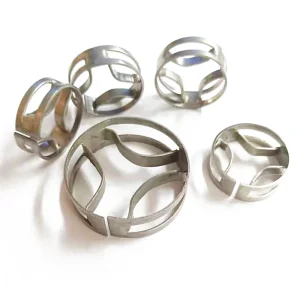
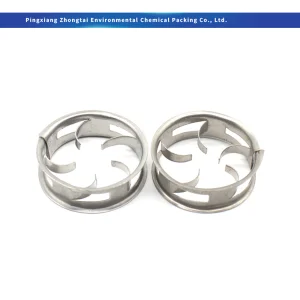
Industrial plants recovering isopropyl alcohol (IPA), ethyl acetate, and bio-butanol utilize our specialized molecular sieves and high-efficiency tower packings (such as SS316L Pall Rings and Theta Rings) to handle corrosive, mixed-solvent side streams with maximum thermal efficiency.
Located in Pingxiang, Jiangxi—China’s recognized heartland for chemical packing and ceramic adsorbents—Zhongtai provides uncompromised vertical integration from raw kaolin clay to final calcined sieves.
Key criteria EPC contractors, plant managers, and global sourcing leaders evaluate when selecting molecular sieve suppliers.
Initial purchasing cost accounts for less than 15% of the total life-cycle cost of adsorbent beds. Premium molecular sieves featuring higher crush resistance reduce attrition loss, preventing fines from migrating into downstream boilers, reboilers, and liquid pumps. Longer operational life directly lowers turn-around labor costs and downtime losses.
Balancing pressure drop ($\Delta P$) against mass transfer zone (MTZ) length is crucial. Smaller bead diameters (1.6-2.5 mm) shorten the mass transfer zone, enabling sharp breakthrough curves in compact systems, while larger spherical beads (3.0-5.0 mm) lower system pressure drop in high-velocity vapor reactors.
Adsorbents are extremely hygroscopic. Zhongtai utilizes heavy-duty hermetically sealed metal drums (150kg/drum with inner heat-sealed vapor-barrier foil bags) or 1000kg flexible super-sacks equipped with aluminum moisture-barrier liners to guarantee zero capacity loss during overseas transit and multi-year warehouse storage.
Full international compliance and round-the-clock technical engineering assistance for continuous plant availability.
Global energy and chemical installations operate under strict regulatory frameworks. Zhongtai products comply fully with EU REACH, RoHS, and OSHA industrial safety standards. Furthermore, our dedicated chemical engineering team provides pre-shipment bed design modeling, mass balance calculations, loading supervision guides (dense-loading vs. socket loading), and bed startup protocol consulting.
Expert insights addressing real-world operating, design, and sourcing challenges.
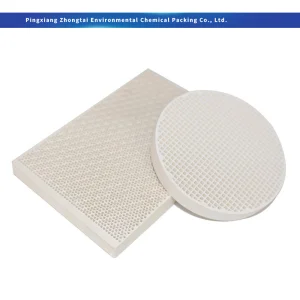
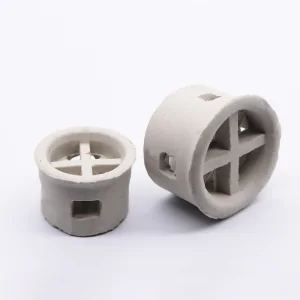
Explore our complete range of high-performance random packings, honeycomb ceramics, and specialized adsorbent media.
Whether designing a new fuel ethanol dehydration unit, retrofitting existing PSA beds, or sourcing high-durability tower packings, our engineering team provides end-to-end technical support, sample testing, and direct factory pricing.
