
High Quality Zeolite 3A Molecular Sieve for Canadian Petrochem Facilities
3Å pore exclusion prevents hydrocarbon co-adsorption. Perfect for fuel ethanol dehydration and LNG pre-treatment plants across Alberta.
View Technical SpecsDirect factory supply of synthetic crystalline aluminosilicates, calibrated specifically for cryogenic gas separation, industrial drying, and gas fractionators.
3Å pore exclusion prevents hydrocarbon co-adsorption. Perfect for fuel ethanol dehydration and LNG pre-treatment plants across Alberta.
View Technical Specs
Pore opening of ~4Å. Exceptional dynamic equilibrium water capacity for closed-loop air compression, paint systems, and refrigerant loops.
View Technical Specs
Calcium-exchanged framework providing excellent N2/O2 separation factors, low attrition rates, and high mechanical crush strength.
View Technical Specs
Type X faujasite structure tailored for large-molecule co-adsorption of CO2, H2O, and lighter hydrocarbons in cryogenic feed air streams.
View Technical SpecsUnderstanding the interplay between sub-zero Canadian processing environments, massive natural gas networks, and global carbon mitigation mandates.
Across Alberta, British Columbia, and Saskatchewan, natural gas sweetening and NGL extraction demand robust adsorbents capable of operating under high pressure without attrition. Sieve bed attrition directly creates fine particulate dust that clogs turboexpanders and heat exchangers in LNG liquefaction corridors.
Canadian pipelines experience severe ambient temperature drops down to -45°C. Water dew point suppression must consistently surpass -100°C (-148°F) to prevent hydrate formation in transport headers, requiring highly specialized Zeolite 4A and 3A molecular sieves with rapid adsorption mass-transfer zones.
Canada's carbon capture, utilization, and storage (CCUS) projects, particularly near Edmonton's industrial heartland, depend heavily on custom 13X APG molecular sieves to scrub low-concentration CO2 and hazardous contaminants before dense-phase CO2 compression and geological sequestration.
Direct comparison of synthetic zeolite frameworks manufactured for pressure-swing adsorption, temperature-swing adsorption (TSA), and specialized gas polishing.
| Zeolite Type | Nominal Pore Diameter | Bulk Density (g/mL) | Static H2O Adsorption (wt%) | Crush Strength (N/bead) | Primary Industrial Sector in Canada |
|---|---|---|---|---|---|
| Zeolite 3A | ~3 Ångströms | 0.68 – 0.74 | ≥ 21.0% | ≥ 85 (3.0mm) | Fuel Ethanol Plants, Cracked Gas, Biofuels, Insulating Glass |
| Zeolite 4A | ~4 Ångströms | 0.66 – 0.72 | ≥ 21.5% | ≥ 90 (3.0mm) | Natural Gas Pipeline Dehydration, Closed Refrigeration Loops |
| Zeolite 5A | ~5 Ångströms | 0.68 – 0.73 | ≥ 21.5% | ≥ 95 (3.0mm) | H2 Pressure Swing Adsorption (PSA), Normal/Iso-paraffin Separation |
| Zeolite 13X / 13X-APG | ~10 Ångströms | 0.64 – 0.70 | ≥ 24.0% | ≥ 80 (3.0mm) | Cryogenic Air Separation Units (ASU), CO2 & H2S Simultaneous Removal |
Our engineered molecular sieves feature narrow particle size distribution, reducing pressure drop while sharpening the Mass Transfer Zone (MTZ). A tighter MTZ allows plant operators to maximize bed capacity and reduce regeneration frequency, yielding direct energy savings during thermal regeneration cycles.
Thermal-swing regeneration up to 300°C can cause lattice collapse in lower-tier sieves. Our clay binder formulations are enriched with specialized kaolin-derived active phases, preserving crystal structural integrity and preventing hydrothermal steaming degradation over 2,000+ operational cycles.
Proven execution methodologies in petrochemical, renewable gas, and mineral processing sectors across Ontario, Quebec, Alberta, and British Columbia.
Renewable Natural Gas (RNG) derived from agricultural digesters and landfills requires deep siloxane, H2S, and moisture removal. Custom 13X-HP and 4A combinations condition the biogas to meet strict Enbridge and Énergir pipeline injection standards.
High-pressure Hydrogen PSA systems utilize specialized 5A and composite zeolite beds to separate synthesis gas streams at 99.999% H2 purity while co-capturing high concentrations of CO2 for downstream deep geological storage.
Remote mineral leaching and smelting sites in the Northwest Territories, Nunavut, and Northern Ontario rely on high-yield Lithium-X and 13X-HP adsorbents to generate continuous, high-volume oxygen on-site without logistical liquid oxygen (LOX) tanker hazards.
Our engineering support team offers adsorption isotherm modeling, vessel dimensioning, pressure drop calculation, and comprehensive customs export clearance for Canadian sites.
Send Inquiry NowComplete product catalog items engineered for heavy refinery turnaround, cryogenics, and separation columns across North American industrial networks.
Engineered with elevated N2 adsorption capacity and rapid mass transfer coefficient, optimizing power efficiency in compact PSA units.
View Technical Specs
Specially prepared for ASU front-end prepurification to simultaneously remove moisture and carbon dioxide down to ultratrace levels.
View Technical Specs
Delivers ultra-low dewpoint protection against hydrate formation across long-distance pipelines and sub-zero gathering stations.
View Technical Specs
Engineered molecular sieve beads for normal-paraffin separation and hydrogen purification units in refinery hydrocracking complexes.
View Technical Specs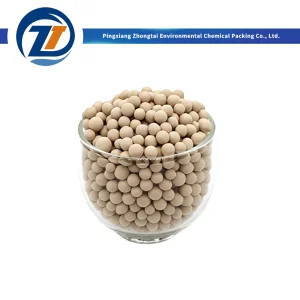
High dynamic capacity for trace hydrocarbons, mercaptans, and carbon dioxide before deep cryogenic liquefaction stages.
View Technical Specs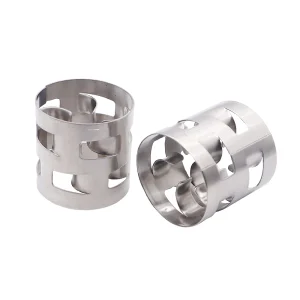
Premium SS304/SS316L random packing delivering superior hydraulic capacity, uniform liquid distribution, and low pressure drop.
View Technical Specs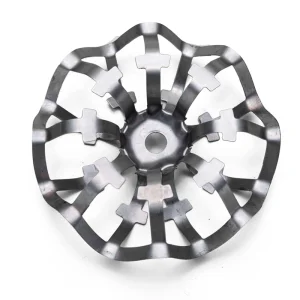
Multi-filament toroidal geometry engineered for particulate interception, gas scrubbing, and mist elimination in chemical plants.
View Technical Specs
Factory-direct batch certified adsorbent with verified crush strength, bulk density consistency, and airtight maritime container packing.
View Technical SpecsKey information regarding material validation, logistics to Canadian ports, hydrothermal regeneration, and performance guarantees.
Whether you require a full bed reload for a refinery turnaround or technical sizing for a new PSA air separation plant in Canada, our engineers are ready to assist with detailed specs and competitive factory pricing.