
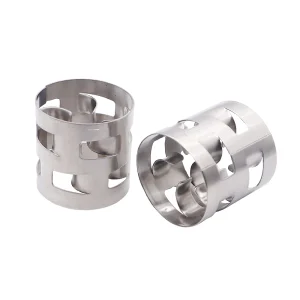
Direct factory-manufactured random media engineered for extreme duty across refining, petrochemical gas scrubbing, and chemical fractionation.
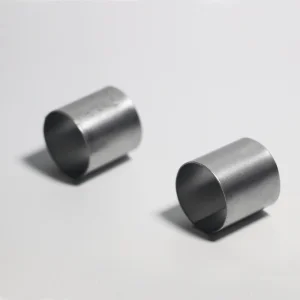
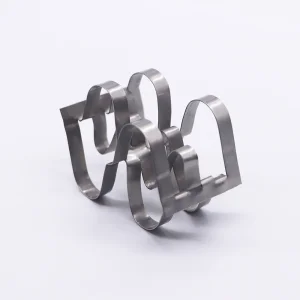
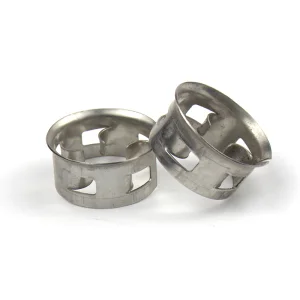
Analyzing the shift from legacy refining to low-carbon hydrogen, offshore platform retrofits, and Net Zero decarbonization projects.
The United Kingdom's major clusters—including the Humber Industrial Cluster, Net Zero Teesside, and HyNet North West—are currently leading multibillion-pound investments in post-combustion Carbon Capture, Utilisation, and Storage (CCUS). Large absorption and stripping columns operating in these installations demand ultra-low pressure drop random packing and high-surface wire gauze packing (such as 316L and 904L alloys) capable of handling massive flue gas volumes with minimal energy consumption.
Offshore installations in the North Sea operate under stringent footprint and weight boundaries. Triethylene Glycol (TEG) contactors and sour gas amine scrubbers demand packing materials engineered from high-grade austenitic and duplex alloys that combine superior mass transfer efficiency with corrosion immunity against high-chloride marine environments and sour sour gas (H₂S/CO₂) conditions, mitigating unwanted tower shutdowns.
Across processing corridors in Grangemouth, Cheshire, and South Wales, specialty chemical producers and high-purity pharmaceutical manufacturers require high-separation-stage structured column packings. With tight vacuum distillation tolerances, low HETP (Height Equivalent to a Theoretical Plate) and precise chemical passivation become mission-critical to avoid product discoloration and catalyst poisoning.
Optimizing hydraulic capacity, reducing column pressure drop, and ensuring thermodynamic efficiency under aggressive UK process conditions.
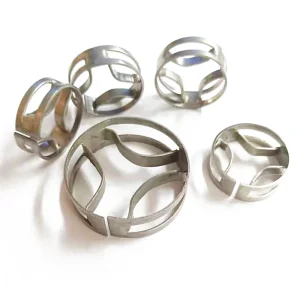
By engineering specialized open-frame geometries like the Cascade Mini Ring (CMR) and Super Raschig Ring, our packings optimize gas-liquid interaction by minimizing stagnant liquid zones. This aerodynamic opening lowers tower pressure drops by up to 35% compared to legacy Raschig rings, offering substantial energy conservation for large blower-driven amine contactors.
We manufacture using globally verified coils of SS304, SS304L, SS316, SS316L, 321, Monel 400, Hastelloy C-276, Titanium Gr. 2, and 2205 Duplex Stainless Steel. Every production run undergoes automated spectrometer chemical analysis, ensuring strict adherence to ASTM A240 and British Standard BS EN 10088-2 requirements with zero carbon contamination.
Our R&D collaborates with leading chemical separation laboratories to conduct multi-phase CFD simulations. These studies model liquid film turbulence, wetting angles, and vapor shear stress across various liquid-to-gas (L/G) ratios, providing process designers in the UK with accurate data for HETP prediction in complex hydrocarbon distillations.
Direct from Pingxiang, Jiangxi—the global capital of mass transfer media—to Felixstowe, Southampton, and Liverpool.
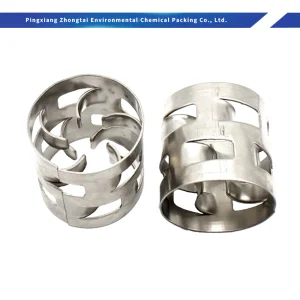
Our production floor operates over 45 high-speed automated mechanical presses equipped with continuous progressive stamping toolsets. This guarantees consistent strip blanking, clean slot formation, and perfectly uniform louver tongues on Pall and VSP rings, eliminating mechanical stress cracks and raw burrs that compromise liquid re-distribution.
With an annual processing capacity of over 15,000 tons of alloy tower internals and structured wire packing, we offer unmatched scale. Large project turnarounds involving multi-column revamps can be completely produced within 2 to 3 weeks, mitigating expensive plant turnaround delays for UK plant managers and maintenance engineers.
By eliminating multiple layers of European trading houses and intermediaries, Zhongtai delivers authentic manufacturer pricing directly to UK end-users. We manage FOB, CIF, and DDP contracts with real-time container tracking to the ports of Felixstowe, Southampton, London Gateway, and Grangemouth.
Stringent quality assurance aligned with Pressure Equipment Directives (PED), UKCA certifications, and environmental criteria.
Every delivery is bundled with comprehensive Material Test Reports (MTR) detailing chemical analysis and mechanical tensile testing for heat-specific traceability. We routinely facilitate third-party verification by SGS, Bureau Veritas, or TÜV Rheinland before container sealing.
Tower packings are packaged in reinforced, water-repellent jumbo bags with dual lifting loops or in heavy-duty reinforced corrugated cartons securely strapped to ISPM-15 heat-treated fumigated wooden pallets, engineered to survive long ocean transits and wet dockside conditions.
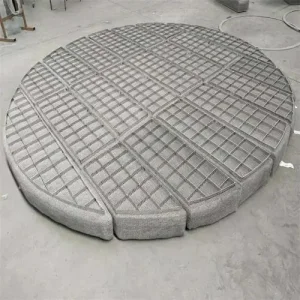
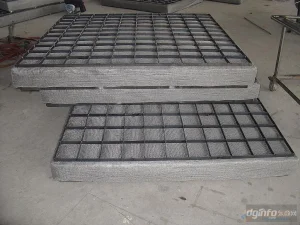
Our dedicated mass transfer team reviews process parameters including reflux ratios, vapor density, foaming tendencies, and fouling factors to verify the exact geometry and size—such as recommending structured wire gauze over random rings when low pressure drop is required.
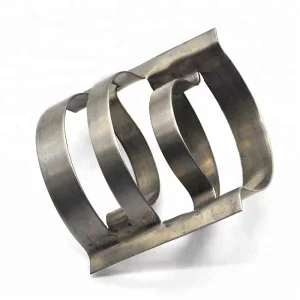
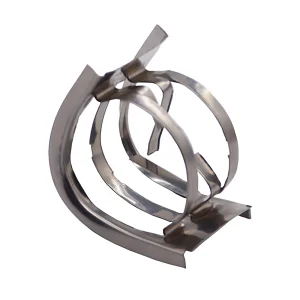
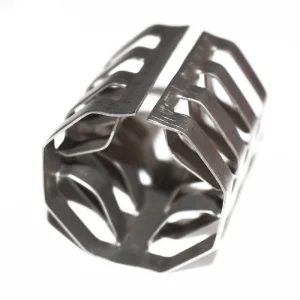
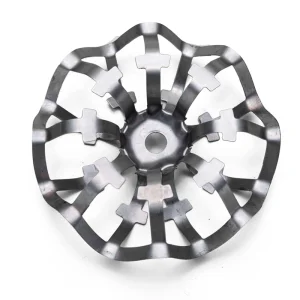
Discover our comprehensive collection of random saddles, high-surface rings, and structured wire gauze packs manufactured for international export.
Clear engineering answers concerning materials, hydraulic parameters, lead times, and British standards.
Contact our chemical mass transfer engineering team for technical evaluations, hydraulic sizing, packing factor sheets, or sample packs dispatched to your UK office.